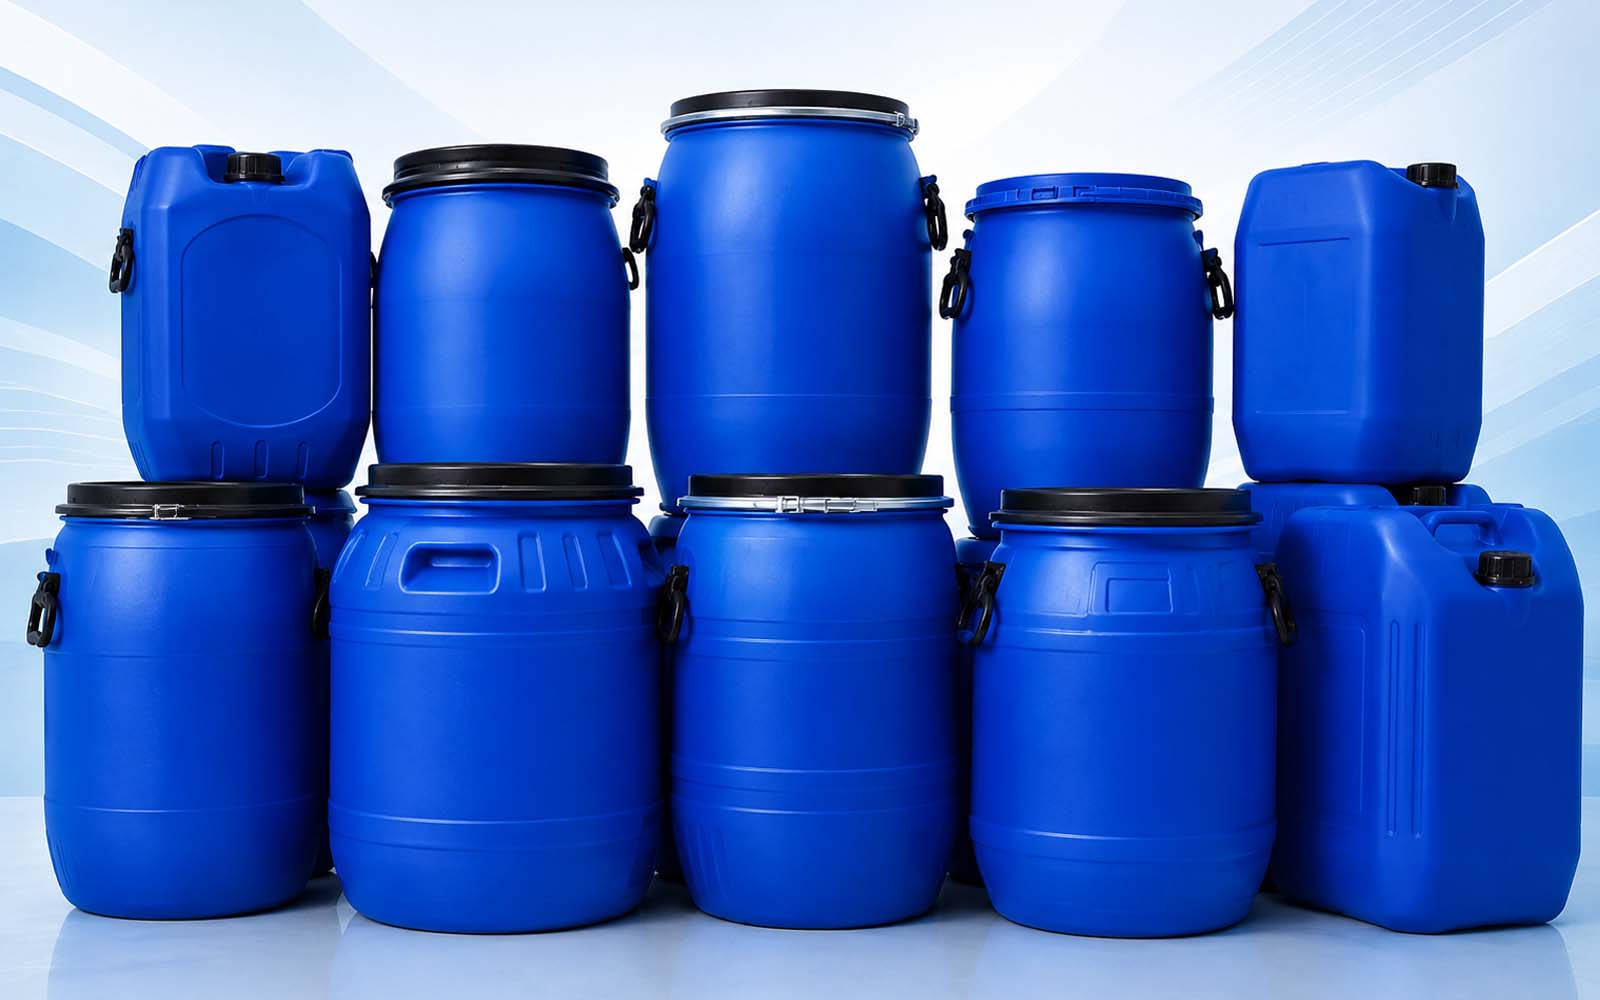
Founded with a vision to deliver safe, durable, and innovative packaging solutions, Ideal Packaging Industries has grown into a trusted name in the manufacturing of HDPE Carboys and industrial packaging products. we combine advanced technology, skilled craftsmanship, and sustainable practices to meet the diverse needs of our clients across industries.
With years of experience and a commitment to excellence, we specialize in producing high-quality packaging that ensures product safety, reliability, and environmental responsibility. Our products are widely used in pharmaceuticals, chemicals, food processing, and FMCG sectors, where quality and compliance are paramount.
At Ideal Packaging Industries, we believe packaging is more than protection-it's a promise of trust. Every product we deliver reflects our dedication to precision, innovation, and customer satisfaction.
Founder and Managing Director of Ideal Packaging Industries
Mr. Kushal Ghatole, Founder and Managing Director of Ideal Packaging Industries, is the driving force behind the company's success. With a strong background in Mechanical Engineering & MBA in Operations Management, he combines technical expertise with strategic vision to lead the company toward excellence.
With a vision rooted in innovation and integrity, he has transformed Ideal Packaging Industries into a trusted name in HDPE Carboy manufacturing.
Starting with a small setup, his dedication and forward-thinking approach have built a company known for quality, reliability, and customer satisfaction. Under his leadership, Ideal Packaging Industries has embraced modern technology, sustainable practices, and a customer-first philosophy.
He believes that packaging isn't just about containers-it's about protecting value, ensuring safety, and building trust. His hands-on involvement in operations, product development, and client relationships reflects his commitment to excellence and continuous growth.
Beyond business, he encourages teamwork, ethical practices, and innovation-values that define the company's culture and success.
To be the most trusted and innovative provider of HDPE Carboy solutions, ensuring safe, sustainable, and reliable packaging for industries worldwide.
Every lot of raw material as well as finished goods go through rigorous and strictly monitored quality control parameters and tests. Any lot thereafter not compiling with our parameters is not used in the production or dispatch. Our every dispatch is attached with a Certificate of Analysis (CoA) report
We undertake drop one from each side i.e. top, bottom & body portion to ensure total safety of your product during transit
Immediately after the drop test, the drum must be rolled on the rough surface to ensure there is no leakage from any part especially from the mouth portion of the drum.
Drum filled with material was kept one + 2 to ensure to see total pressure on the drum kept on the surface
We undertake air pressure test to see there is no leakage from the closures & Seams.
Our containers also undergo running trial to ensure that they can perform efficiently after the shipment.